

1. Aluminum Alloy Composition
Different aluminum alloys respond differently during anodizing.
For example:
- 6061 Aluminum produces a consistent and attractive anodized finish.
- 7075 Aluminum may appear darker due to its higher zinc content.
- 2024 Aluminum often develops uneven coloring because of its copper content.
- Cast aluminum may show visible color inconsistency due to its silicon content and casting structure.
Even small differences in alloy composition can affect dye absorption and oxide layer formation.
2. Surface Finish Before Anodizing
The final anodized appearance depends heavily on the surface preparation before anodizing.
Different machining or finishing methods produce different surface textures:
- CNC machining marks
- Sandblasting
- Glass bead blasting
- Brushed finish
- Polishing
Although parts receive the same anodizing treatment, different surface roughness reflects light differently, making the color appear lighter or darker.
3. Oxide Layer Thickness
The thickness of the anodic oxide layer significantly affects color.
A thicker oxide layer absorbs more dye, while a thinner layer absorbs less.
Factors influencing oxide thickness include:
- Anodizing time
- Current density
- Voltage
- Electrolyte temperature
Maintaining stable process parameters is essential for color consistency.
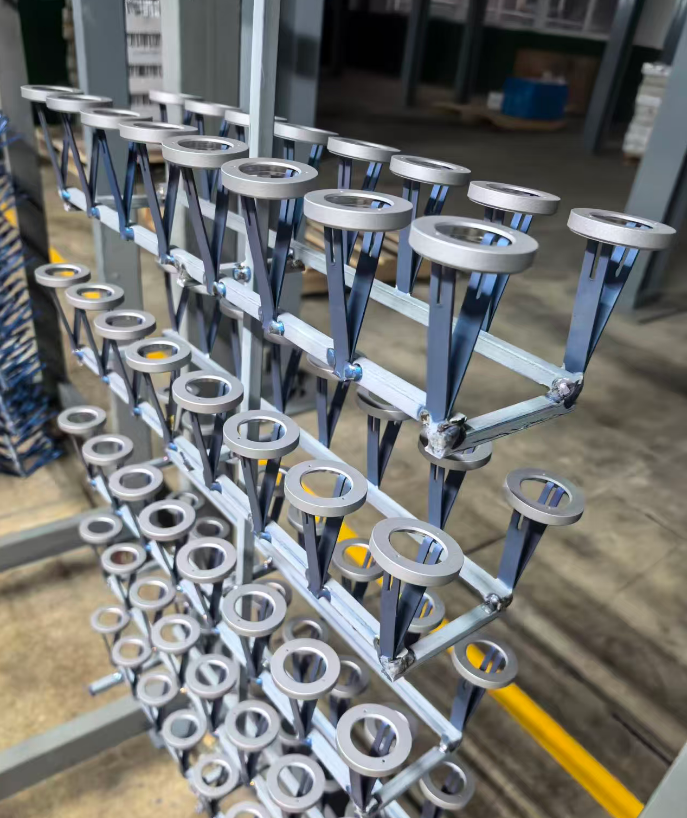
4. Dye Concentration and Dyeing Time
For colored anodizing, the dyeing process is critical.
Color variation may result from:
- Dye concentration changes
- Dye bath aging
- Different immersion times
- Bath contamination
Professional anodizing suppliers regularly monitor and replenish dye baths to maintain stable color performance.
5. Batch-to-Batch Production
Even with identical specifications, parts anodized in different production batches may show slight color differences.
This is because:
- Process parameters may vary slightly.
- Environmental conditions can change.
- Dye baths gradually age over time.
For cosmetic products, it is often recommended to anodize all visible components in the same production batch.
6. Part Geometry
Complex part shapes may anodize differently.
Features such as:
- Deep pockets
- Thin walls
- Sharp corners
- Large flat surfaces
can experience different current distribution during anodizing, resulting in slight color variation across the same part.
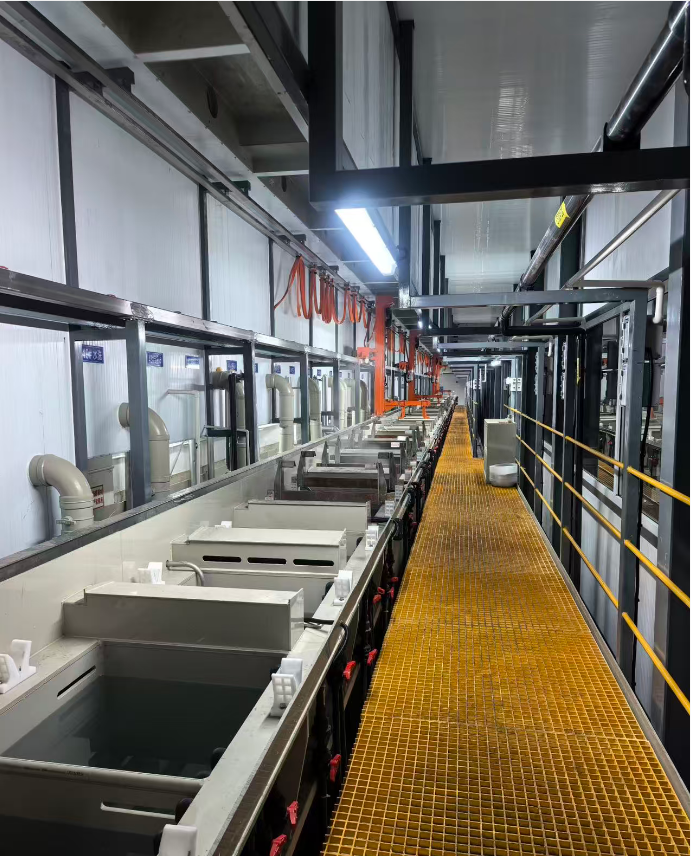
7. Temperature Control
Anodizing is highly sensitive to temperature.
Variations in electrolyte or dye bath temperature can influence:
- Oxide growth rate
- Dye absorption
- Surface appearance
Professional anodizing facilities use strict temperature control systems to ensure process stability.
8. Sealing Process
After dyeing, anodized parts are sealed to improve corrosion resistance.
Improper sealing may lead to:
- Uneven color
- Reduced gloss
- Lower corrosion resistance
- Dye fading over time
A properly controlled sealing process helps maintain long-term color stability.
How to Reduce Color Variation
Although it is impossible to eliminate all color variation, manufacturers can significantly improve consistency by:
- Using the same aluminum alloy for all parts
- Maintaining consistent surface preparation
- Processing cosmetic parts in the same anodizing batch
- Strictly controlling anodizing parameters
- Working with experienced anodizing suppliers
- Performing color inspection before shipment